
STEP 1Order / RFQSend quantity & requirement
Verified supplier
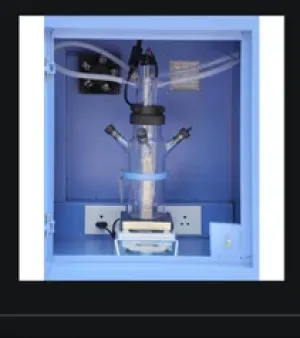
Lab Photochemical Reactor, Application : Reaction
Category: Photochemical Reactor
Secure payment optionsChoose how you want to pay
UPI
Cards
NetBanking
Bank Transfer
STEP 2Supplier ConfirmsStock, price & dispatch
STEP 3DeliveryTrack shipment to destination
✓ Secure enquiry✓ No payment required✓ Direct supplier response
PRODUCT DETAILS
Everything you need before you source
Review overview, specifications and supplier information in one clear product workspace.
Buyer-ready information
Product overview
The Lab Photochemical Reactor is a cutting-edge device designed for precise and efficient photochemical reactions. Engineered for both research and industrial applications, it features an advanced light source—often UV or visible spectrum—capable of delivering controlled and uniform illumination to reaction samples. The reactor includes adjustable reaction vessels, integrated cooling systems, and precise temperature controls to maintain optimal conditions. Its intuitive control panel allows users to set and monitor reaction parameters, ensuring reproducibility and accuracy. Built with high-quality materials for durability, the Lab Photochemical Reactor supports a wide range of photochemical experiments, including synthesis and degradation processes. Ideal for chemists and researchers, it offers a reliable platform for exploring light-driven reactions and advancing scientific discoveries.
Direct supplier enquiryYour requirement goes straight to the listed supplier.
Commercial clarityConfirm quantity, specification, lead time and delivery before ordering.
Buyer protectionNo payment is required to request the latest quotation.
Specifications
Specifications are available from the supplier on request.
About the supplier
Established in the year 2002, we Unity Glass Industry, are one of the leading organizations engaged in manufacturing and supplying a wide range of Spherical Vessels, Laboratory Valves, Laboratory Equipment and many more. All our products are made using best quality raw material such as borosilicate glass and other essential raw material. Being crack-resistant, heat resistant and chemical resistant, our offered products find applications in chemical plants, pharmaceutical industry and hospitals. Apart from this, our products are used for storing Bulk Drugs and for conducting various experiments in Laboratories of schools and colleges. We are backed by a sound infrastructure and a competent workforce. This helps us in executing our endeavors in a smooth and proper way. Optimizing the use of cutting edge technology, we are able to bring forth the offered range within the specified time limit. For the ultimate satisfaction of our clients, we thoroughly check the products at each and every stage of production. We hold expertise in offering customized products as per the specifications detailed by the clients along with the facility of OE and private labeling on each products. Owing to our ethical business practices and cordial approaches towards our clients, we have established a huge client base across the nation. Our list of clientele incorporates some prominent names such as Alembic Ltd., Zyfine Cadila Group, Amoli Organics, Reliance Industries, Bodal Group, Amneal Pharma Ltd, Apicore Pharmaceuticals Pvt. Ltd, Tonira Pharma Group and IPCA Laboratories. Under the able and efficient guidance of our mentor Mr. V. C. Rohit, we have been able to position ourselves among the leading manufacturers of the industry. His ninteen years of industry experience motivates us to put our best effort to achieve maximum client satisfaction.
More options
Related products
Photochemical Reactor, Material : GLASS AND QUARTZ
₹1,00,000.00 / Units
A photochemical reactor is a specialized apparatus designed to facilitate and optimize photochemical reaction…
MOQ 10
⌖ Vadodara, Gujarat, India
✓ Verified
Unity Glass Industry
✓
PHOTO REACTOR APPARATUS, Material : Stainless Steel
₹88,000.00 / Units
The Photo Reactor Apparatus is a sophisticated system designed for advanced photochemical reactions and exper…
MOQ 10
⌖ Vadodara, Gujarat, India
✓ Verified
Unity Glass Industry
✓
Photochemical Reactor, Application : Industrial
₹1,00,000.00 / Units
A photochemical reactor is a specialized apparatus designed to facilitate and optimize photochemical reaction…
MOQ 10
⌖ Vadodara, Gujarat, India
✓ Verified
Unity Glass Industry
✓