
STEP 1Order / RFQSend quantity & requirement
Verified supplier
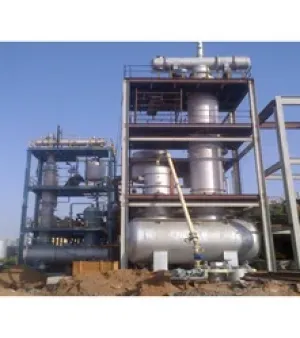
Chemical Process Technology Equipment, Application : Chemical Industry
Category: Chemical Equipment
Secure payment optionsChoose how you want to pay
UPI
Cards
NetBanking
Bank Transfer
STEP 2Supplier ConfirmsStock, price & dispatch
STEP 3DeliveryTrack shipment to destination
✓ Secure enquiry✓ No payment required✓ Direct supplier response
PRODUCT DETAILS
Everything you need before you source
Review overview, specifications and supplier information in one clear product workspace.
Buyer-ready information
Product overview
Chemical process technology equipment encompasses a range of devices and systems used to conduct, control, and optimize chemical processes in industrial settings. This equipment includes reactors, separators, distillation columns, heat exchangers, and mixers, each designed to facilitate specific stages of chemical production. Reactors provide controlled environments for chemical reactions, while separators and distillation columns are used for purifying and separating components. Heat exchangers manage temperature by transferring heat between fluids, and mixers ensure thorough blending of ingredients. Additionally, pumps, valves, and sensors are integral for fluid handling and process monitoring. This equipment is essential in industries such as pharmaceuticals, chemicals, and petrochemicals, ensuring efficient, safe, and precise production. Adherence to quality standards and regular maintenance are crucial for optimal performance and safety.
Direct supplier enquiryYour requirement goes straight to the listed supplier.
Commercial clarityConfirm quantity, specification, lead time and delivery before ordering.
Buyer protectionNo payment is required to request the latest quotation.
Specifications
Specifications are available from the supplier on request.
About the supplier
Incorporated in the year 2009, we, “ Acme Process Systems Pvt Ltd.”, are counted amongst the leading manufacturers and suppliers of a remarkable range of Industrial Vessels, Industrial Reactors, Distillation Systems, Column Internals, Industrial Tanks, etc to serve our clients in best possible manner. Apart from this we also provide Chemical Industries Turnkey Projects to our customers. The products offered by us are known for their special design, high production capability, resistance to corrosion, rust and abrasion, low power consumption and reliability for a long-lasting performance. We manufactured these products with premier-grade raw material and implementing latest technologies to ensure optimum client satisfaction. For streamlined execution of our business operations, we have established an advanced infrastructure. Our infrastructure is well-equipped with sophisticated tools, equipment and machineries which are utilized by our diligent professionals for manufacturing the offered product line. We have also appointed experts and developed advanced R&D cell to provide turn-key solutions in this area. Our professionals ensure that the products and solutions offered by us must be qualitative as per the international quality standards. For the same, offered products manufactured with quality-assured raw material and solutions are executed under the surveillance of our dexterous experts. Offered solutions and products are valuable for our clients to gain to achieve their specific goals and highest level of productivity. For our client-centric approach, we have been able to win the loyalty of various clients like Thermax Limited, Pune, Maharashtra, Akzo Nobel Paints, Chandigarh, Alafa Laval (India) Limited, Pune, Maharashtra and many others.
More options
Related products
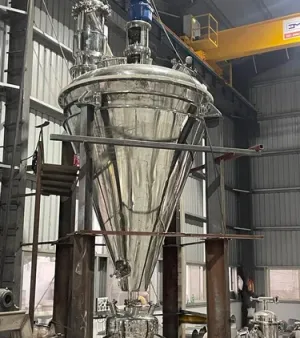
Conical Blender Machine, Type : Customized
₹50,000.00 / Units
A conical blender machine is an industrial equipment designed for efficient mixing and blending of powders an…
MOQ 10
⌖ Pune, Maharashtra, India
✓ Verified
Acme Process Systems Private Limited.
✓
Promac Process Equipment for Industrial Use
₹50,00,000.00 / Units
Promac Process Equipment is a leading manufacturer specializing in high-quality equipment for various industr…
MOQ 10
⌖ Pune, Maharashtra, India
✓ Verified
Acme Process Systems Private Limited.
✓
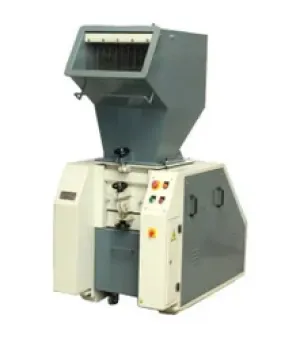
Mild Steel Automatic Plastic Processing Plants
₹50,000.00 / Units
Mild Steel Automatic Plastic Processing Plants are industrial facilities designed for the automated productio…
MOQ 10
⌖ Pune, Maharashtra, India
✓ Verified
Acme Process Systems Private Limited.
✓